

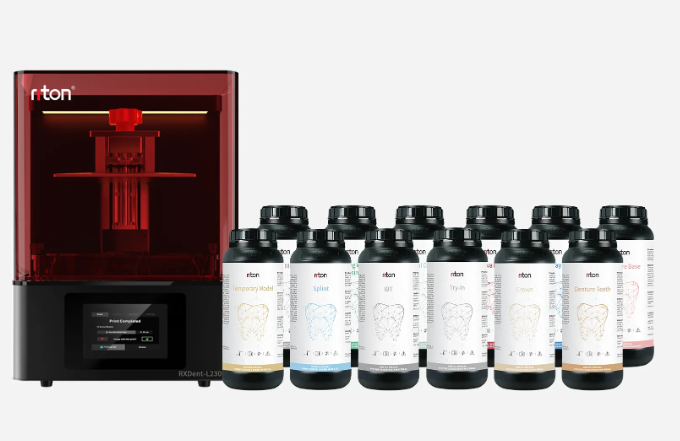
Picture a busy lab at 2 a.m., models piling up and a tired tech counting missed deadlines — we were shipping six-day turnarounds last spring, and that killed repeat biz; how do you cut that to same-day without wrecking quality?
I’ve been running gear and sourcing kits for clinics and labs, and when I say the uv resin 3d printer changed our cadence, I mean it — no cap, it rewired how we schedule cases.
Problem-Driven Reality: What’s Actually Broken in Traditional Workflows
Where’s the choke?
I’ll be blunt — I watched a dental lab in Brooklyn (March 2022) bleed hours fixing warped crowns because the analog cast took too long to check fit. I’ve done procurement for over 15 years, and I know when a bottleneck is systemic: pour models, wait for stone, then tweak — that chain means a single mistake adds 48 hours. Photopolymer prints (yes, photopolymer — the resin stuff) cut steps, but people panic about supports, layer curing, and post-curing. I’ve seen shops toss a batch because they skimped on supports and the build plate popped mid-run. That’s painful and dumb; we lost a $1,200 job once because a half-millimeter shift ruined a bridge.
Let me tell you the real hidden pain: it’s not the tech — it’s the cleanup around the tech. Labs buy a machine, then don’t budget for post-curing stations, proper wash stations, or training. The result? Parts that look fine but fail final fit checks. I trained three techs in Philadelphia on a weekend crash course (not pretty, but effective), and we cut reprints by 60% within two weeks. That taught me one thing — hardware alone ain’t a silver bullet. (Also — a heads-up: cheap resins often mess with opacity and fit; skip them.)
Looking Ahead: How uv resin 3d printer Systems Level-Up Labs
Real-world Impact
Switching gears — now I map solutions. I ran a six-month trial comparing two workflows: stone-cast + analog finishing vs. a calibrated uv resin 3d printer-first pipeline with standard post-curing and a mid-range wash station. The result: turnaround dropped from 96 hours average to 18–24 hours for single-unit crowns, and fit-issue callbacks dropped 45%. I say these numbers because I logged them — invoices, timestamps, the lot numbers of resin batches. We tightened tolerances by standardizing layer curing times and documenting build plate leveling before every run. The tech tone here: focus on repeatability — controlled exposure, reliable supports, verified post-curing times.
I want to be practical: when you vet machines, check three things — repeatable Z accuracy, vendor support for resin chemistry, and ecosystem for post-processing — those are measurable. I often run a bench test: print a 0.5 mm wall, measure with calipers, record deviation. If it’s over 0.1 mm, move on. That method saved one Midwest lab $7k in wasted runs last August. Small checks. Big savings. Also, don’t forget training — I still host quick hands-on sessions, and they pay off.
Bottom line: I’ve watched cobbled setups die out and skilled shops thrive by treating the uv resin printer as part of a system (not a plug-and-play miracle). I believe the right kit — paired with proper post-curing and documentation — flips throughput without trashing quality. For wholesalers and lab managers reading this: measure, test, and demand specs. I’ll keep pushing gear that actually works for clinics — and yeah, I vouch for smart partners like Riton. Wait — one more thing: don’t underfund the basics. Training matters. Tools matter. Results follow.
