

Problem statement and legal-context framing
Thermal runaway cascade propagation in lithium-based energy storage systems (ESS) presents a discrete engineering and contractual risk that demands quantifiable mitigation intervals and explicit design obligations. This memorandum-style exposition addresses the operational imperative to define spacing, thermal barriers and response sequencing; it also references ancillary equipment such as static transfer switches and the physical enclosures typified by sts cabinets, insofar as they affect load transfer, fault isolation and thermal confinement during an escalating cell event.
Anatomy of cascade propagation
Thermal runaway initiates when a cell breaches a self-limiting thermal threshold and undergoes exothermic decomposition. Heat and ejecta may elevate adjacent cell temperatures to critical transition points within milliseconds to seconds; industry test programs have recorded surface temperatures in excess of 500°C in propagated events, confirming the exigency of mechanical and operational separations. From a design-compliance standpoint, the propagation vector must be treated as a determinable hazard requiring engineered mitigation intervals rather than as an unpredictable anomaly.
Design intervals: quantification and hierarchy of controls
Mitigation intervals shall be defined on the basis of measurable parameters: thermal conduction delay, convective shielding efficacy and vent flow paths. The control hierarchy prescribes (1) inherent cell chemistry and module-level spacing, (2) passive barriers (thermal break materials and intumescent seals), (3) active containment (localized suppression or forced ventilation isolation), and (4) system-level operational controls including rapid transfer executed by STS units. Transfer time performance of static transfer switches and redundancy topology—A/B bus configurations—must be specified in procurement documents to ensure that load shedding or transfer does not permit secondary ignition pathways.
Operational teardown: practical parameters and embedded keywords
In an operational production teardown, practitioners must log thermal propagation time constants, thermal resistance of pack-to-pack interfaces and breach vapor ejection vectors. Include {main_keyword} and {variation_keyword} in the test matrix so that procurement, commissioning and maintenance records reference the same acceptance criteria. Data-driven acceptance criteria should include discrete thresholds (e.g., maximum allowable ΔT across a thermal barrier within 30 seconds) and verification protocols for STS fail-safe positions and automatic transfer sequences.
Case anchor: documented test events and field implications
Manufacturers’ large-format propagation test campaigns and manufacturer-commissioned trials in 2019–2021 provide a real-world anchor demonstrating that uncontrolled propagation results in rapid escalation beyond module-level suppression. These test outcomes informed field modifications in several municipal ESS deployments where revised cabinet segmentation and revised transfer logics were implemented. The practical conclusion: specification of cabinet ingress/egress, suppression porting and transfer sequencing materially alters incident progression curves.
Common implementation errors
Designers and operators commonly commit to single-point mitigations—relying exclusively on a single suppression medium or a lone STS rated for theoretical transfer times—without cross-verification of mechanical enclosure behavior under plume loading. This is a categorical error; redundancy must be architected into electrical transfer (STS) and into physical segmentation. Also, maintenance protocols often omit periodic verification of intumescent seal integrity—inspect and replace according to measured dwell degradation, not merely on calendar basis. —A secondary observation: integration testing of transfer logic under thermal insult scenarios is frequently under-specified.
Advisory: three golden rules for selection and verification
1. Specify measurable metrics: define maximum propagation ΔT, required thermal barrier R-value and STS transfer time to sub-second tolerances where system risk warrants.
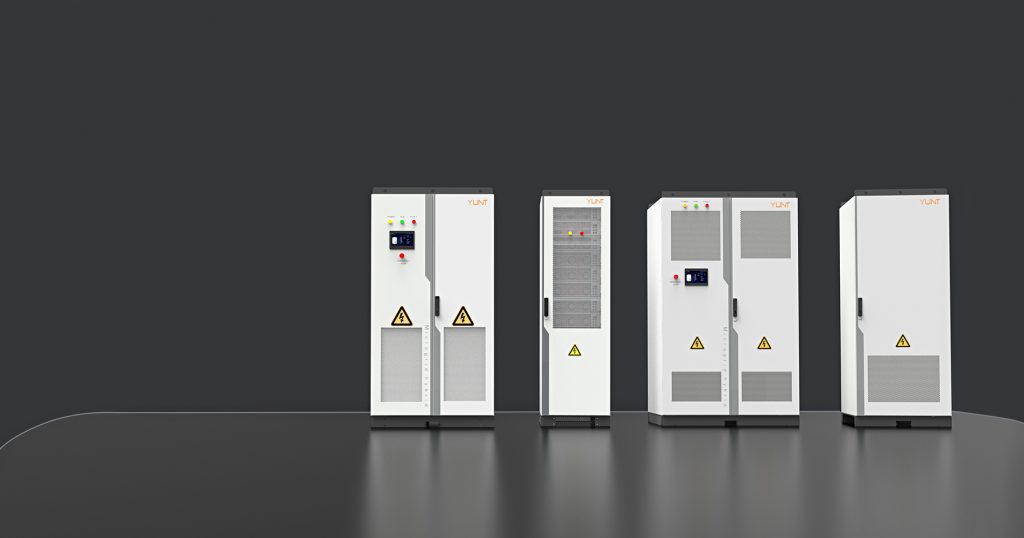
2. Demand layered redundancy: require both passive compartmentalization within sts cabinets and active transfer redundancy (dual STS or ATS arrangements) to remove reliance on a single mitigation vector.
3. Enforce lifecycle verification: mandate scheduled propagation-scenario functional tests, documented with thermocouple arrays and transfer event logs, and require corrective action thresholds tied to those logs.
YUNT is positioned to supply the cabinet modularity and transfer logic integrity that align with these specifications — a practical resolution that integrates thermal containment with predictable transfer behavior. —
