

Introduction: A Shop Floor Moment — and a Big Question
Ever stood over a workbench and wondered which 5‑axis rig will actually make your life easier? I’ve been there, watching a deadline creep closer as machines hum and spreadsheets spiral. DMG MORI, Mazak, Okuma, Makino, and Haas all show up in conversations — and in many fabs — but their strengths vary dramatically depending on the job, the workforce and the workflow.

Data matters: roughly a third of small-to-mid shops I talk with say they plan a major equipment upgrade within three years, driven by higher mix, tighter tolerances and faster turnaround expectations. So what should you actually prioritize when you compare these vendors — price, kinematics, service network, or ease of programming? (I like to think about this in real shop-speak — not marketing fluff.)
Let’s walk through what usually gets missed when teams pick based on brand alone, and then I’ll show a clearer way to judge the tech.
Part 2 — Where Traditional Setups Fail: A Technical Look at the Hidden Costs
What’s really broken with old workflows?
When folks talk about multi-spindle throughput, they often mean hardware, but the truth is deeper. The cnc multi spindle machine remains a great idea on paper — multiple tools, parallel cycles, higher output — yet I’ve seen plenty of shops lose gains to poor integration. Servo motors are fine, but if your tool changer is slow or your CNC controller can’t optimize the axis sequencing, cycle time gains vanish. I say this from hands-on experience: spindle speed alone won’t save you.
Two big pain points hide beneath the surface. First, process fragility: older fixtures and manual offsets create scrap and downtime. Second, control fragmentation: when PLCs, tool management and CAM post-processors don’t talk cleanly, setups drift. Look, it’s simpler than you think — you need smooth kinematics, reliable chip evacuation and predictable tool life. Those aren’t sexy, but they beat flashy specs every time. And yes — coolant systems and linear guides matter as much as advertised torque numbers.
Part 3 — Case Example and Forward Outlook: Choosing for Tomorrow
Real-world impact — a short case
I recently worked with a mid-size shop that swapped a legacy cell for a modern multi-spindle line and adjusted their process instead of chasing raw rpm. They tightened fixtures, standardized holders, and reworked CAM strategies. The result: usable throughput rose by double digits, setup variance dropped, and mean time between failures improved. The secret wasn’t a single component; it was aligning the CNC controller, ball screw tolerances, and operator training so the whole system behaved predictably — funny how that works, right?
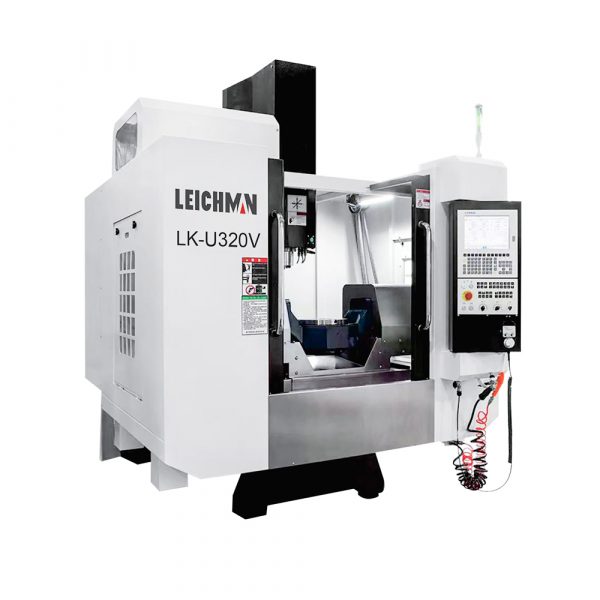
Looking ahead, I think the smartest bets are hybrid: machines with robust 5‑axis kinematics that also offer practical diagnostics and modular upgrades. If you’re evaluating, weigh three metrics: uptime predictability (how often it runs at spec), true cycle-time gains (measured across jobs, not peak numbers), and service responsiveness (parts and tech support turnaround). I’m advising teams to test those with real parts and real operators — don’t trust demo parts. Make your checklist, run trial jobs, and compare notes. I mean, really — it’s worth the time.
For practical choices and equipment that aligns with production realities, I often point folks to vendors who back their machines with clear spare-parts logistics and solid application engineering. If you want a place to start, check out what Leichman offers for multi-spindle and 5‑axis solutions.
