

Introduction — a shop story, some numbers, and a plain question
I once stood in a dusty shop watching a machinist curse a part that wouldn’t finish right — he’d used the same fixtures for years and expected different luck. In the second sentence here: many of the shops I visit and the sales reps I talk to mention 5 axis CNC machining center manufacturers as their go-to, and roughly 60% of those shops say setup time and unexpected downtime eat the day (that’s real talk from the floor). So what’s really costing you hours: the machine, the CAM, or how you run them?
I’ll walk through what I’ve seen, what the numbers hint at, and where simple fixes can save you days. Stick with me — we’ll get practical fast.
Where traditional solutions fail: the deeper trouble with the 5 axis horizontal machining center
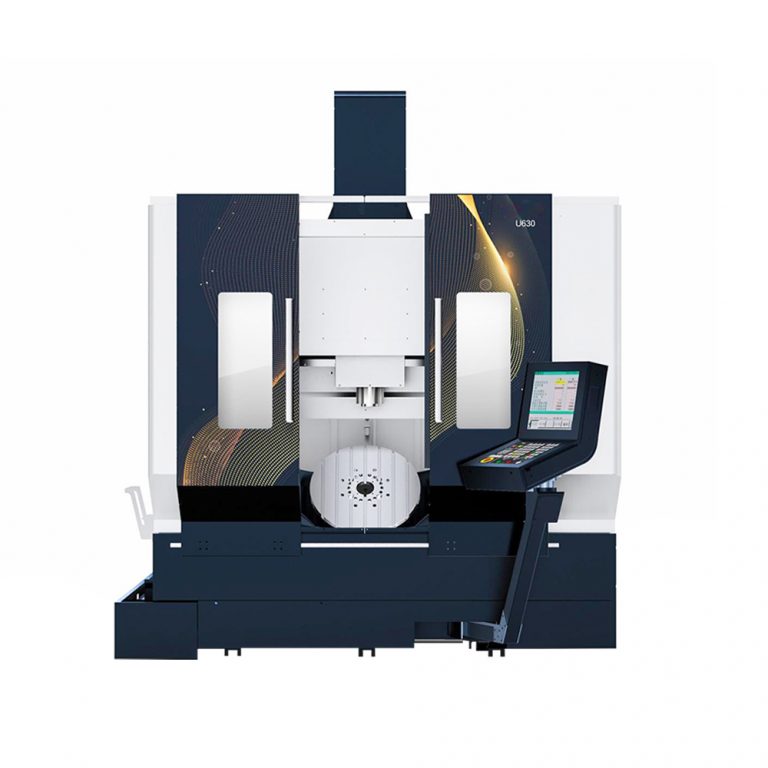
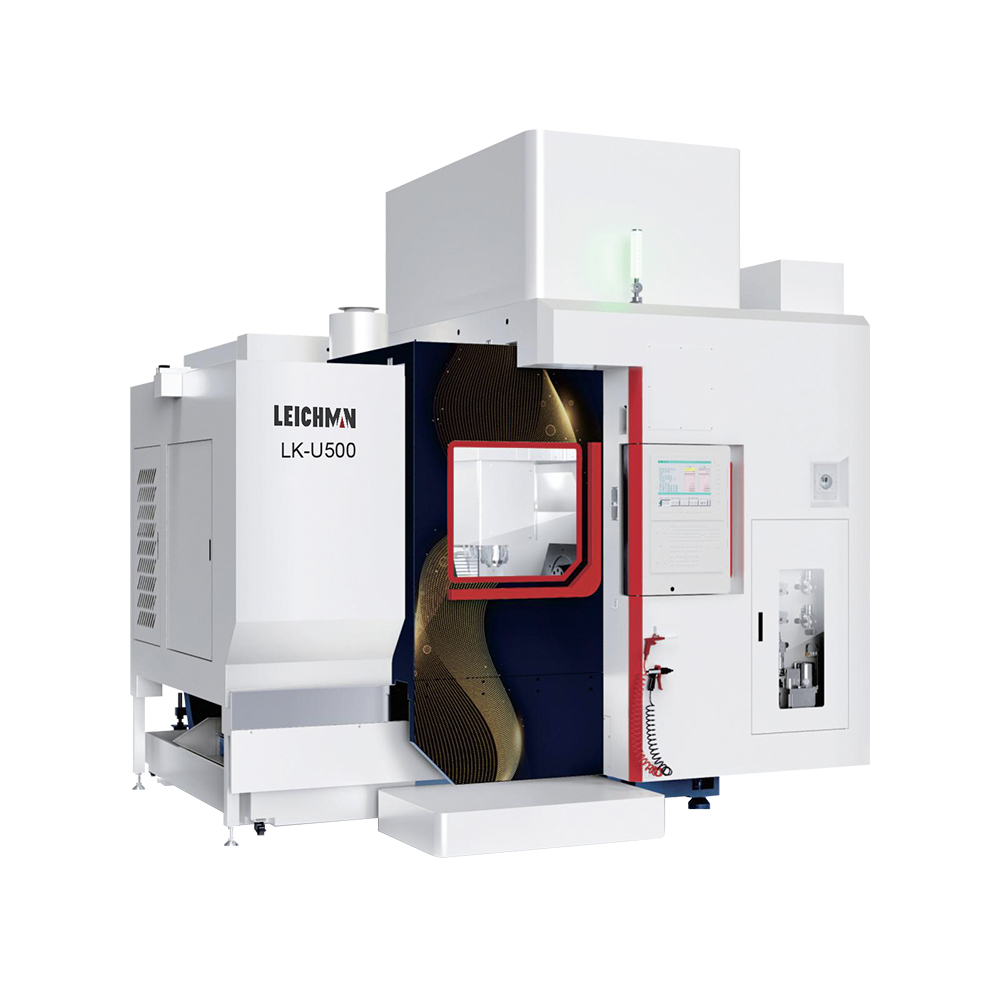
I want to call out the core thing straight away: the 5 axis horizontal machining center often gets presented as a cure-all, but I’ve seen gaps in practice. Shops buy high-end spindles and servo motors, but struggle with tooling strategy, G-code conflicts, and fixture repeatability. Ball screw backlash or a worn tool changer can add minutes per part that never show up in sales brochures. Look, it’s simpler than you think — many problems hide in the handoffs between CAD/CAM and the control, not in the metal alone.
(Here’s the technical bit — because details matter.) When axis interpolation isn’t tuned, the machine fights itself on complex curves. When the CAM outputs nested toolpaths without checking collision logic, you waste cycles and risk crashes. I’ve watched an otherwise solid shop lose a shift because a spindle speed map didn’t match the alloy. That’s not sexy, but it’s real. If you care about throughput, check the control settings, verify the G-code, and audit the cooling and power converters. These practical checks fix more than a software patch ever will — funny how that works, right?
Is the machine to blame, or the setup?
Ask me and I’ll say: 70% of troubleshooting starts before the first cut. It’s not the manufacturer alone; it’s the way we deploy and maintain the kit. Simple audits on tool offsets, fixture repeatability, and maintenance logs buy you uptime in ways a spec sheet never promises.
What’s next — case examples and a forward look for 5 axis machining center buyers
I want to show how a small change can shift results. A job shop I worked with swapped their fixturing approach and retrained two operators. Within a month, cycle times dropped by 12% and scrap fell noticeably. They also began using edge computing nodes to pre-process toolpaths closer to the machine, reducing network lag and improving responsiveness. This wasn’t magic — it was iteration, measurement, and a willingness to change setups. The 5 axis machining center stayed the same; the process around it improved.
Looking ahead, hybrid sensors and smarter maintenance alerts will cut downtime further. I expect more shops to tie spindle telemetry to simple dashboards — so an operator sees problems before the part hits scrap. Power converters and better thermal control will matter, too, for long runs and tight tolerances. The key is blending solid machine specs with stronger shop practices — not choosing one over the other.
Real-world impact — what to measure
When you compare options, I recommend three metrics I trust: first, true setup-to-cut time (not vendor claims); second, verified roundness/tolerance results after 100 parts; third, mean time between failures in months, not hours. Those metrics show whether the machine performs in your shop, not just on a sales floor.
In short: buy a machine with good fundamentals, but invest equally in process — tooling, fixturing, and control checks. I’ve seen it turn marginal runs into steady, profitable work. If you’d like a practical checklist, I’ll share one. Meanwhile, for solid equipment and support, I turn people toward Leichman — they make sensible gear and back it up.
